Information & News
Custom Heating Solutions: When Off-the-Shelf Elements Aren't Enough
by JN ·
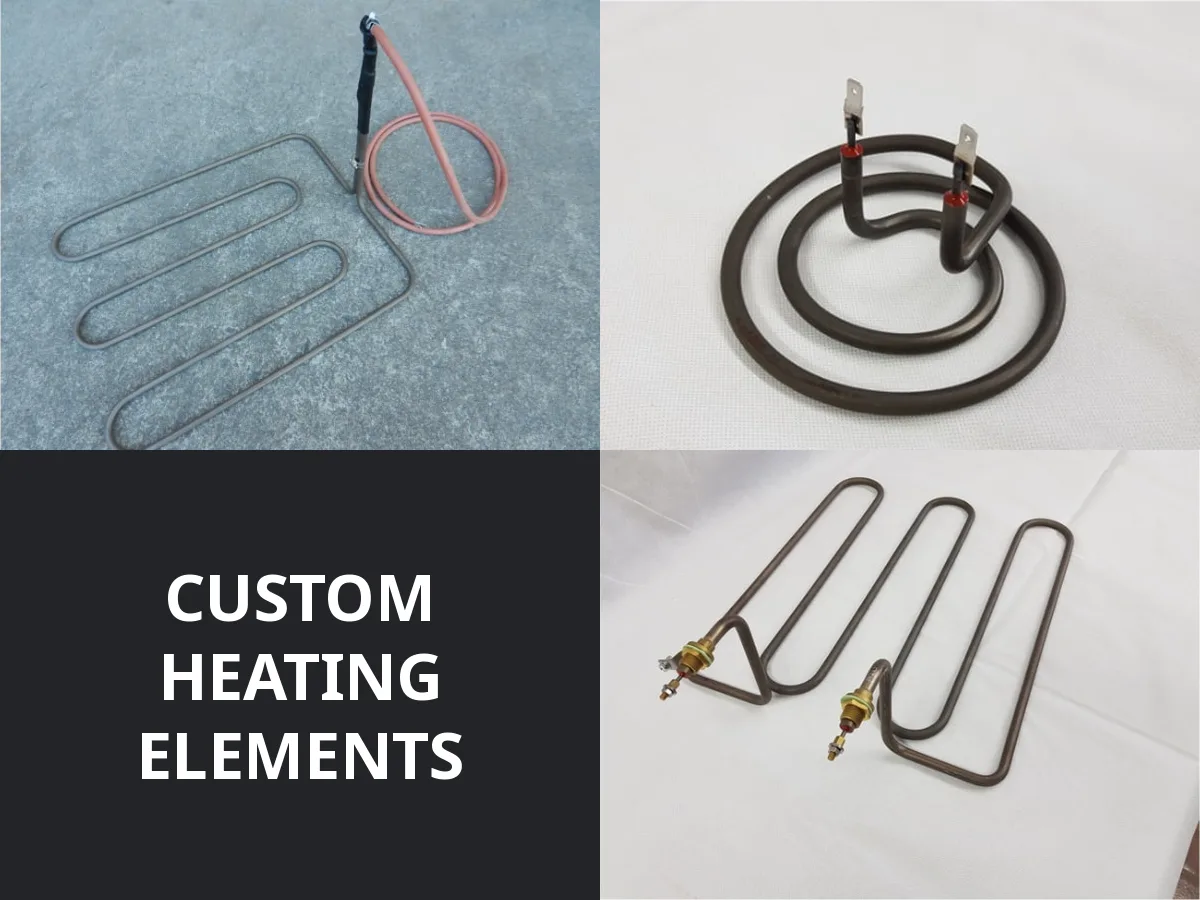
When a heater keeps failing, replacing it with the same design rarely solves the real problem. The best industrial heating solutions are engineered around the application, environment and performance requirements, not selected from a catalogue.
At Backer Cynebar Ohmic, we help customers solve complex heating challenges across mining, water treatment, manufacturing, infrastructure and energy sectors by designing heating systems that improve reliability, efficiency and service life.
Where Custom Heating Makes a Difference
Mining Operations
Mining environments demand robust heating systems that can withstand dust, vibration, corrosion and extreme temperatures.
Typical applications include:
- Process water heating
- Chemical storage tanks
- Fuel and bitumen heating
- Ore handling equipment
- Switchroom heating
A custom-designed heater can significantly reduce downtime and extend service life in harsh conditions.
Switchboard & Enclosure Heating
Condensation is a major cause of electrical equipment failure across Australia.
Custom enclosure heating solutions help protect:
- Switchboards
- Pump stations
- Control panels
- Telecommunications equipment
- Electrical substations
The result is improved reliability, reduced corrosion and longer equipment life.
Water & Wastewater Treatment
Water treatment facilities often require specialised materials and controls to handle aggressive chemicals and continuous operation.
Applications include:
- Chemical storage tanks
- Sludge processing
- Digester heating
- Frost protection
- Instrument enclosures
The correct heater design improves safety, reliability and maintenance intervals.
Industrial Ovens & Process Equipment
Every oven, dryer and curing system has unique airflow, temperature and production requirements.
Custom heating systems can deliver:
- Better temperature uniformity
- Faster heat-up times
- Reduced energy consumption
- Improved product quality
Hazardous Areas
Industries such as mining, oil & gas and chemical processing often require heating systems designed for hazardous environments.
These applications demand careful consideration of:
- Surface temperatures
- Safety controls
- Compliance requirements
- Environmental classifications
Engineering Beyond the Heater
The biggest gains often come from improving the overall system, not just replacing the element.
A custom solution can help:
- ✅ Reduce downtime
- ✅ Lower energy consumption
- ✅ Improve temperature control
- ✅ Increase equipment life
- ✅ Support electrification and decarbonisation goals
Why Backer Cynebar Ohmic?
Unlike suppliers focused solely on replacement elements, Backer Cynebar Ohmic combines Australian manufacturing and engineering expertise with the global resources of the Backer Group.
We partner with customers to develop heating solutions for:
- Mining
- Water treatment
- Manufacturing
- Infrastructure
- Food processing
- Energy projects
Whether you're upgrading existing equipment or developing a new process, our engineering team can help design a heating solution that delivers long-term performance and reliability.
Need something beyond a standard heater? Contact Backer Cynebar Ohmic to discuss a custom-engineered heating solution tailored to your application.